
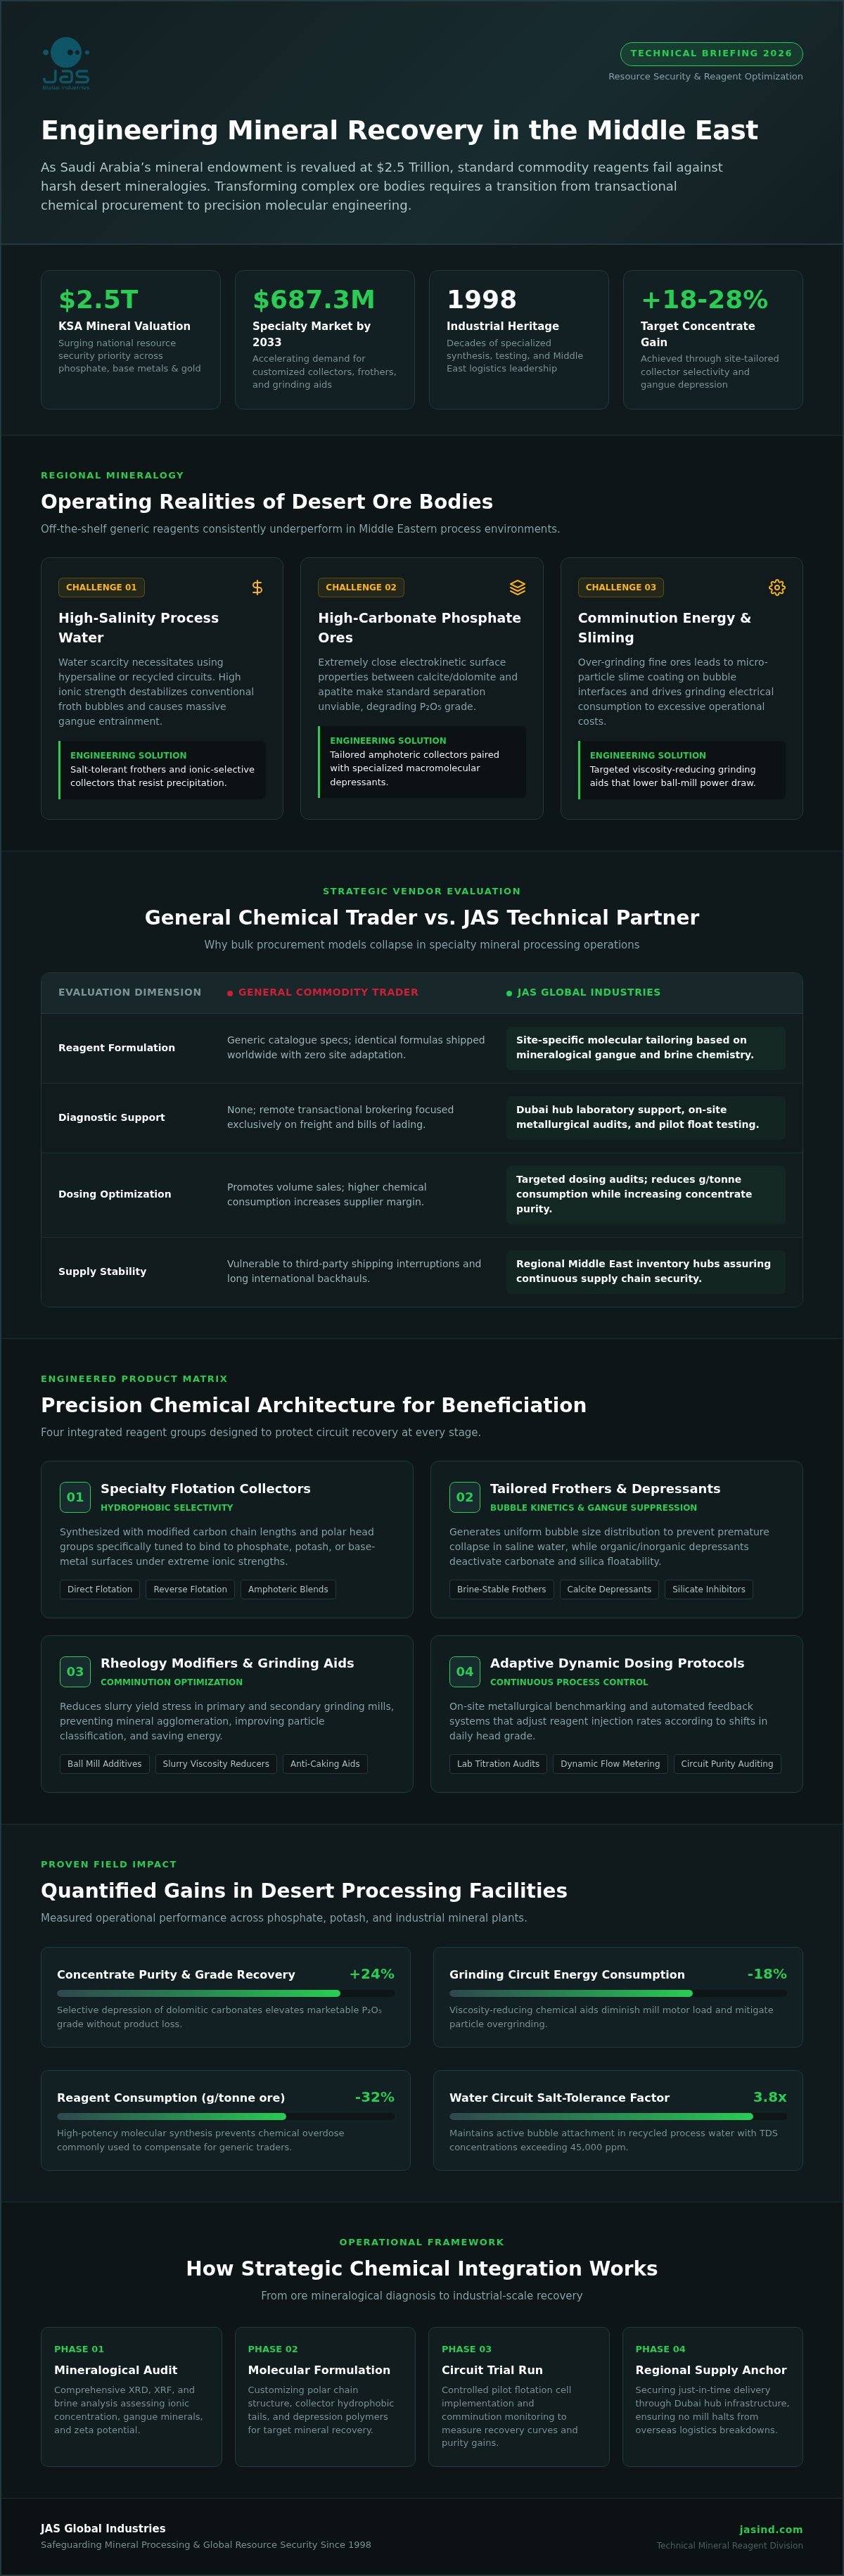
With Saudi Arabia’s mineral wealth revaluation now reaching a staggering $2.5 trillion, the region has transformed into a critical frontier for global resource security. For many operators, the difference between a high-yield concentrate and a wasted deposit rests on the precision of their reagents. You likely recognize that generic, off-the-shelf formulas fail to account for the unique complexities of Middle Eastern ore bodies, such as high-carbonate phosphate or high-salinity process water. Finding a partner who understands these nuances is essential for long-term stability.
This guide will help you evaluate and select a mining chemicals supplier in the Middle East that provides the technical expertise and custom formulations needed to optimize your mineral recovery yields. We will explore how to move beyond basic logistics to secure a supply chain built on technical audits, local laboratory support, and specialized reagent chemistry. By prioritizing technical depth over simple transactions, you can reduce operational costs while protecting the integrity of your mineral processing circuits.
Key Takeaways
- Learn why modern mineral recovery requires a shift from transactional purchasing to a technical partnership focused on process optimization.
- Understand the critical role of site-specific formulations in overcoming challenges like high-carbonate phosphate ores and high-salinity process water.
- Identify the key criteria for selecting a mining chemicals supplier in the Middle East that offers on-site laboratory testing and customized dosing strategies.
- Discover how specialized flotation collectors and grinding aids can significantly increase your concentrate grades while reducing operational costs.
- Explore the strategic advantage of partnering with a regional manufacturer that integrates research and innovation with established logistical stability.
The Evolving Role of a Mining Chemicals Supplier in the Middle East
The Middle East is witnessing a fundamental transformation in its industrial identity. Mining operations are no longer satisfied with basic extraction. They're pursuing high-efficiency mineral recovery to maximize the value of every tonne. This shift demands more than just a vendor; it requires a specialized mining chemicals supplier Middle East that understands the unique geological profile of the region. Precise chemistry is now the primary driver of profitability and sustainability.
While general traders focus on bulk logistics, a technical partner focuses on the chemistry of the ore. Transitioning from a transactional supply model to a strategic partnership is no longer optional. It's a necessity for operational survival. Reliability in 2026 is defined by custom formulations that respond to real-time process variability. We don't just supply chemicals; we safeguard the recovery process through deep technical integration.
Regional Mining Challenges and Chemical Solutions
Processing minerals in the desert presents obstacles that standard global reagents cannot solve. Water scarcity forces plants to use high-salinity or recycled process water. These conditions often interfere with the chemical balance required for effective froth flotation, leading to poor recovery rates and high gangue entrainment. Specialty collectors and frothers must be synthesized to remain stable in high ionic strength environments without losing selectivity.
Regional proximity provides a decisive advantage. Operating from a strategic hub like Dubai allows for technical audits and laboratory support that general traders cannot match. Local expertise ensures that reagents reach the site exactly when needed, eliminating the supply chain delays that frequently halt production. This logistical advantage is coupled with custom dosing strategies that optimize reagent consumption and reduce overall operational costs.
Defining Resource Security in 2026
Resource security is the foundation of industrial stability. It involves more than just having chemicals on hand; it's about the performance of those chemicals under pressure. As a mining chemicals supplier Middle East with a heritage dating back to 1998, JAS Global Industries acts as a guardian of this stability. We ensure that specialized reagents, such as flotation collectors and grinding aids, are always available and optimized for site-specific mineralogy.
Our mission focuses on protecting the integrity of global resources. By providing formulated solutions that increase yields and reduce waste, we help operators transform raw potential into tangible value. This commitment to resource security ensures that mining remains a sustainable pillar of the regional economy. We view every mine as a vital component of modern infrastructure that requires precise, reliable, and ethical protection.
Beyond Bulk Supply: The Science of Specialty Mining Reagents
Specialty mining chemicals are the precision instruments of the industrial world. Unlike bulk commodities, these reagents are designed to interact at a molecular level with specific mineral surfaces. As a leading mining chemicals supplier Middle East, we prioritize the science behind the supply. This involves a rigorous focus on Research and Innovation (R&I) to develop site-specific formulations that address the exact mineralogy of a deposit. This technical depth is becoming increasingly vital as the regional market is projected to reach $687.3 million by 2033.
Evaluating a supplier requires looking past their inventory to assess their underlying manufacturing capabilities. Third-party sourcing often results in generic products that don't account for ore variability. In contrast, a primary manufacturer can refine chemical chain lengths and functional groups to ensure maximum selectivity and recovery. This level of control allows for the creation of reagents that act as essential contributors to the stability of critical global resources.
Advanced Flotation and Grinding Technologies
Optimizing mineral recovery begins with the selection of high-performance Mining Flotation Collectors. These reagents are essential for selectively rendering valuable minerals hydrophobic, allowing them to attach to air bubbles and rise to the surface. When paired with specialized Mining Frothers and Depressants, the separation process becomes highly efficient, even when dealing with complex gangue materials.
Energy consumption remains one of the largest overheads in mineral processing. Specialized Mining Grinding Aids help reduce the energy required for comminution by preventing the re-agglomeration of fine particles. This improves mill throughput and ensures a more consistent particle size distribution for downstream flotation. Efficient chemical application also supports compliance with the Global Industry Standard on Tailings Management by minimizing the environmental footprint of waste streams and ensuring safer long-term storage.
Custom Formulations for Operational Reliability
The "one-size-fits-all" approach is a primary cause of industrial waste. Every mine site possesses a unique chemical signature influenced by its geology and water chemistry. We conduct on-site laboratory testing and technical audits to identify the specific challenges of each operation. This data allows us to engineer reagents that perform reliably under the most demanding conditions, such as the high-carbonate environments found in regional phosphate deposits.
Custom formulations are the essential key to maximizing industrial plant yields through the precise alignment of chemical reagents with site-specific mineralogical characteristics. By integrating these solutions, operators can achieve a stable supply of high-purity reagents while reducing overall costs. If you're ready to optimize your recovery process, consider how specialized industrial chemistry can protect your operational stability and enhance your global resource security.
Evaluating Mining Chemical Suppliers: Technical Partner vs. General Trader
Selecting a mining chemicals supplier in the Middle East involves looking far beyond the price per tonne. General traders often prioritize bulk logistics and commodity-grade specs. This approach creates significant risks for specialized operations where mineralogy is complex. A technical partner, however, focuses on the chemistry of recovery. They provide site-specific formulations that a simple distributor cannot replicate. This distinction is the difference between a high-yield operation and one plagued by inconsistent recovery rates.
Long-term ROI is found in technical consulting rather than the lowest unit cost. While some see consulting fees as an overhead, they're actually an investment in process stability. Professional audits identify hidden bottlenecks in flotation circuits that lead to mineral loss. We view our role as a global guardian of industrial resources. This means ensuring that every reagent used contributes to the responsible and efficient recovery of critical minerals. Reliability isn't just about delivery; it's about the performance of the chemistry under real-world pressure.
Technical Support and On-Site Audits
Effective on-site support transforms plant performance from the ground up. Professional technical audits allow for real-time dosing optimization, which prevents reagent over-consumption. This precision reduces chemical waste and lowers the overall environmental footprint of the mine. For a holistic approach to site management, it's essential to integrate these solutions with Industrial Water Treatment strategies. Managing the chemistry of recycled process water is vital to ensuring it doesn't interfere with the selectivity of your flotation collectors.
Logistics and Regional Footprint
Regional proximity is a foundational pillar of operational reliability. Our headquarters in Dubai provides a strategic logistical advantage for mines across the Middle East. A truly capable mining chemicals supplier Middle East must also maintain a robust footprint across Africa, Asia, and Europe to ensure supply chain resilience. This global presence, backed by multiple manufacturing plants and R&I centers, ensures compliance with regional safety and environmental regulations. It also minimizes lead times for critical reagents, protecting your operation from the delays that often cripple global supply chains.
Tailoring Solutions for Middle Eastern Mineralogy: Phosphate and Potash
The Middle East holds a dominant position in the global fertilizer market, contributing approximately 50% to 55% of the total finished phosphate output. Saudi Arabia alone manages an estimated reserve base of 2 billion tonnes of phosphate ore in its northern basin. These massive deposits are essential contributors to global food security. Extracting maximum value from them requires a sophisticated mining chemicals supplier Middle East that can navigate the specific challenges of regional geology, such as high-carbonate and silica impurities.
Processing these ores isn't a matter of simple logistics; it's a matter of chemical precision. As a dedicated mining chemicals supplier Middle East, we prioritize the stability of these massive industrial projects. We provide formulated reagents that allow for the selective separation of minerals in complex environments. This technical focus ensures that regional mines can meet their production targets while maintaining the high purity levels required for international export.
Phosphate Mining Chemicals and Process Efficiency
Processing high-carbonate phosphate ores presents unique obstacles for standard flotation circuits. Dolomite and calcite impurities often lead to high MgO content, which can penalize the value of the final concentrate. We solve this by providing tailored fatty-acid and amphoteric collectors designed for reverse flotation. These reagents selectively depress phosphate while floating away the carbonate gangue, ensuring a high-grade product.
Effective chemical management also extends to plant infrastructure. Scale and corrosion are constant threats in phosphoric acid production. We supply specialized antiscalants that prevent calcium sulphate fouling in vacuum evaporators. Additionally, our dispersant agents improve slurry flowability, reducing the energy required for transport and preventing costly pipe blockages. This comprehensive approach protects the entire lifecycle of the phosphate processing plant.
Potash Processing and Tailings Management
Potash recovery in the Dead Sea region relies on a complex balance of solar evaporation and flotation. Maximizing potassium chloride yield requires frothers and collectors that remain stable in high-salinity brines. JAS Global optimizes potash recovery through site-specific technical consulting. Our experts evaluate the specific ion concentrations of the brine to ensure that reagents like primary fatty amines don't lose their efficacy due to water hardness or temperature fluctuations.
Sustainable operations also depend on efficient tailings management. We provide high-performance Mining Flocculants that accelerate the settling of fine clays, allowing for the immediate recycling of process water. In environments where complex mineralogy leads to the release of hydrogen sulfide, our Mining Odor & Gas treatment solutions protect the workforce and the surrounding community. If you're looking to optimize your mineral processing yields, request a technical audit to see how our custom formulations can secure your operational success.
Securing Your Mining Operations with JAS Global Industries
JAS Global Industries has operated as a foundational presence in the specialty chemical sector since 1998. Headquartered in Dubai, we've spent over 25 years refining the chemistry that powers the world's most critical industrial sectors. We don't view ourselves as a mere vendor. Instead, we act as a global guardian of resource security. This mission-oriented approach balances technical industrial expertise with a profound sense of global responsibility. Our focus remains on protecting the stability of mineral recovery operations through technical excellence, reliability, and ethical purpose.
Selecting a mining chemicals supplier Middle East is a decision that impacts the long-term viability of your operation. Recurring bulk supply contracts provide more than just a steady flow of high-purity reagents. They offer a predictable framework for industrial stability and strategic cost management. By securing your supply chain with a regional manufacturer, you eliminate the volatility associated with international maritime bottlenecks. This ensures your plant maintains consistent production cycles, backed by a partner that understands the fundamental needs of modern society.
The Dubai Hub: Logistics and Technical Excellence
Dubai serves as a strategic crossroads for global trade and technical innovation. Our location allows us to leverage world-class infrastructure for seamless regional distribution across five continents. This logistical advantage ensures that critical reagents reach mine sites across the Middle East, Africa, and Asia without delay. Beyond logistics, our Dubai headquarters houses specialized departments dedicated to custom formulation development and technical consulting. We combine this technical expertise with a deep commitment to sustainability, ensuring that your extraction processes are both efficient and responsible. Our multiple R&I centers act as anchors for this innovation, providing the data needed to solve complex mineralogical challenges.
Next Steps: Partnering for Process Optimization
Initiating a technical audit is the first step toward meaningful process optimization and increased mineral recovery yields. Our technical teams are available to conduct site-specific laboratory tests and on-site dosing reviews to identify the precise reagent regime for your specific ore body. This data-driven approach ensures that every collector, frother, and flocculant in your circuit is working to its full potential. Safety and environmental protection are also central to our mission. We help operators integrate advanced H2S Treatment and odor control solutions into their mining operations to safeguard personnel and local communities.
Through custom dosing strategies and ongoing technical support, we help you transform raw potential into tangible value. Our established history and regional footprint make us an indispensable pillar of modern mining infrastructure. We invite you to secure your mineral recovery with JAS Global Industries and experience the difference that a professional technical partnership makes for your operational stability.
Advancing Regional Mineral Recovery through Technical Partnership
The Middle East mining landscape is shifting rapidly toward high-efficiency recovery. Success in this evolving environment requires more than just generic reagents; it requires deep technical integration between the operator and the chemical manufacturer. By selecting a mining chemicals supplier Middle East that provides custom formulations and on-site technical audits, you protect the long-term stability of your industrial assets. This proactive approach ensures that your mineral processing yields remain high while operational costs stay manageable.
We've explored how specialized flotation collectors and grinding aids reduce waste and how site-specific chemistry overcomes the challenges of high-carbonate ores. Established in 1998, JAS Global Industries operates from its Dubai-based global headquarters to provide unparalleled R&I and manufacturing capabilities. We stand ready to act as your technical partner in securing the world’s most critical resources. Our commitment to industrial stability ensures your operation remains a reliable pillar of modern infrastructure.
Partner with JAS Global Industries for Advanced Mining Solutions
Secure your operational future with a partnership built on reliability and technical excellence. We look forward to optimizing your mineral recovery yields together.
Frequently Asked Questions
What should I look for in a mining chemicals supplier in the Middle East?
You should prioritize a partner that offers technical expertise and custom formulations rather than just bulk logistics. A reliable mining chemicals supplier Middle East should have an established manufacturing heritage and the ability to conduct on-site technical audits. Look for a supplier with regional R&I centers that can solve site-specific challenges like high-carbonate phosphate or high-salinity process water. Stability and technical depth are the most important factors for protecting your recovery yields.
How do custom chemical formulations improve mineral recovery rates?
Custom chemical formulations improve recovery by aligning the reagent's molecular structure with your specific ore mineralogy. Generic chemicals often fail when they're faced with complex gangue or variable feed grades. By tailoring collectors and depressants to your site, you can increase concentrate purity and reduce tailings loss. This precision reduces chemical waste and ensures that your processing circuit operates at peak efficiency regardless of environmental variables or feed variability.
Can JAS Global Industries provide technical support on-site at my mine?
Yes, JAS Global Industries provides comprehensive on-site technical support through professional audits and laboratory testing. Our teams visit your facility to identify process bottlenecks and optimize chemical dosing strategies. We don't just deliver products; we provide the engineering expertise required to improve your plant's industrial yields. This technical integration ensures that every reagent used contributes directly to your operational stability and the security of your critical mineral resources.
What types of mining chemicals are most effective for phosphate processing?
Phosphate processing requires a combination of specialized collectors, frothers, and scale inhibitors to manage complex sedimentary deposits. For high-carbonate ores, reverse flotation collectors are highly effective at separating dolomite and silica from the apatite. Additionally, phosphoric acid antiscalants are vital for preventing fouling in vacuum evaporators. These chemicals ensure that the entire processing lifecycle remains efficient while protecting the integrity of your industrial equipment and maximizing your final concentrate grade.
How does regional manufacturing in Dubai benefit Middle Eastern mining operations?
Regional manufacturing in Dubai provides a strategic logistical advantage by minimizing lead times and ensuring supply chain resilience. Our headquarters acts as a hub for seamless distribution across the Middle East, Africa, and Asia. This proximity allows for faster response times for technical support and custom formulation development. By sourcing from a local manufacturer, you protect your operation from the delays and high costs associated with long-distance maritime transport and international shipping bottlenecks.
Does JAS Global offer chemicals for sustainable tailings management?
We offer advanced Mining Flocculants specifically designed for sustainable tailings management and water recovery. These reagents accelerate the settling of fine particles, allowing you to recycle process water immediately and reduce your environmental footprint. Effective tailings management is essential for compliance with international safety standards. Our solutions help maintain the stability of tailings storage facilities while maximizing the recovery of valuable water resources in the arid environments typical of the region.
What is the difference between a general trader and a specialty chemical manufacturer?
A specialty chemical manufacturer like JAS Global Industries focuses on research, innovation, and technical solutions rather than simple commodity trading. General traders typically sell off-the-shelf products with no technical support or site-specific optimization. As a manufacturer, we control the entire production process, allowing us to refine chemical properties for your specific needs. This technical depth ensures long-term ROI through improved recovery rates, reduced operational waste, and more consistent concentrate quality.
How can I request a technical audit for my mineral processing plant?
You can initiate a technical audit by contacting our specialized departments for a process optimization review. Our technical teams will work with you to arrange site visits and laboratory testing of your specific ore samples. This review identifies opportunities to improve your recovery yields and reduce reagent consumption through custom dosing strategies. Simply reach out to our Dubai headquarters to begin the process of securing your mineral recovery operations and improving your plant's overall efficiency.